Processes: What to Know to Improve Your Manufacturing Workflow
Processes on technical drawings are not decoration—they drive function, cost, lead time, and quality. Reading them reliably lets you batch similar work, select capable suppliers, and avoid costly rework.
Werk24 automatically detects and normalizes process information from drawings so you can:
- Group and route parts by required steps (e.g., turn → mill → anodize).
- Estimate accurately, accounting for heat‑treat, coating thickness, masking, inspection, etc.
- Verify feasibility (e.g., hardness vs. alloy, coating vs. tolerance stack).
Skipping process notes typically increases quoting variance and shop‑floor friction.
How Werk24 reads process information
Werk24 scans Canvas Notes and the Title Block for process language, standards, and numeric outcomes, then emits clean, typed JSON you can act on. Signals include:
- Method keywords: anodize, zinc‑plate, passivate, black oxide, Q&T, anneal, temper, nitriding, induction harden, shot‑peen, tumble, bead‑blast, powder coat, e‑coat, weld, braze, adhesive bond, EDM, grind, hone.
- Outcome specs: 440 HV 30/20, HRC 48–52, Type II Class 2 Black, Fe/Zn‑8, Ra 1.6 µm, case 0.8–1.2 mm.
- Standards (when present): e.g., ISO 6507 (HV), ISO 6508 (HRC), EN ISO 4042 (zinc plating), ASTM A967 (passivation), MIL‑A‑8625 (anodize).
Werk24 normalizes synonyms (e.g., “harden & temper” ↔ “Q&T”) and harmonizes units (µm/mm, HV/HRC) while preserving the raw note for traceability.
Main vs. Post‑Processing
Different organizations draw this line differently. Practically:
- Main processes change the shape or join material: casting, forging, additive manufacturing, bending, milling/turning, grinding, welding/brazing, adhesive bonding, riveting.
- Post‑processing changes properties or surfaces: heat treatment, surface treatments/coatings, finishing, marking, and inspection/testing.
Werk24 outputs a unified
processstructure and, when inferable, tagsstageasmainorpost. If your ERP requires a strict split, map usingfamilyandmethod.
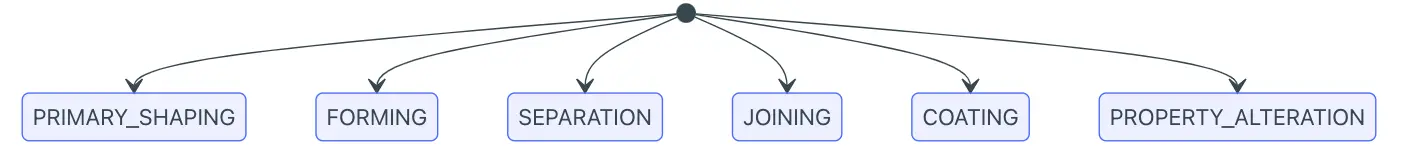
Process families (taxonomy)
| Family | Examples | Typical parameters |
|---|---|---|
| Primary shaping | Casting, forging, extrusion, AM (DMLS/SLS/SLA/FDM) | alloy/grade, net‑shape, heat history |
| Forming | Bending, deep‑draw, rolling | bend angle/radius, K‑factor, springback note |
| Machining | Turning, milling, drilling, grinding, EDM, broaching, honing, lapping | op sequence, tool class, stock allowance |
| Joining | TIG/MIG/MAG welding, brazing, soldering, adhesive, riveting | process, filler, standard, NDT required |
| Heat treatment | Anneal, normalize, quench & temper, stress‑relieve, precipitation harden, induction harden, case harden (carburize/nitriding/nitrocarburize) | hardness & scale, case depth, temperature/profile |
| Surface treatment / coating | Anodize (Type II/III), passivate, zinc/nickel/chrome plate, black oxide, phosphate, galvanize, PVD/CVD, paint/powder coat, e‑coat | thickness, class/color, standard, masking |
| Finishing | Deburr, vibratory tumble, bead‑blast, shot‑peen, polish | intensity/medium, Ra target, edges policy |
| Marking / traceability | Laser etch, stamp, dot‑peen | location, format, size |
| Inspection / testing | CMM, hardness test, pressure test, NDT (UT/MT/PT/RT), leak test | method, class, acceptance criteria |
Best practices for authors of drawings
- Put one process per bullet in General Notes; include standard + class + thickness/hardness.
- For coatings, state masking/no‑coat zones and thickness range in µm.
- For heat‑treat, give target hardness and case/core depth where relevant.
- Avoid unexplained acronyms (HT, HR). Prefer “HRC 48–52 per ISO 6508‑1”.
- If surface finish and coating interact, sequence them (e.g., “grind after heat‑treat; anodize after final machining”).
Process categorization (reference)
Werk24 maintains a controlled vocabulary for processes and synonyms so downstream systems can rely on stable keys. See the live list of currently supported processes and standards: